The Factory Shift Changed. The Machine Problem Didn't.
A practical guide for small manufacturers to carry unfinished production, maintenance and quality issues across shifts without losing responsibility.
Share this article
Browse all insightsIt is 2:45 PM at a small manufacturing factory.
The morning shift is preparing to leave.
One machine has developed an unusual noise.
A production order is incomplete.
The maintenance technician has inspected the equipment but has not yet authorised it to return to service.
The outgoing supervisor tells the incoming supervisor:
There was some problem with Machine 3. Maintenance was checking it. Also, check the pending production.
The evening shift takes over.
The workers see an unfinished production order.
They know that today's target must be completed.
But the handover has not clearly established whether Machine 3 is authorised for operation, what maintenance work remains pending, or who is responsible for obtaining the next update.
The next shift now has a problem that began earlier, without all the information needed to manage it.
The employees have changed. The unresolved issue has not.
For small manufacturers operating two or three shifts, this is an important operational weakness.
Production problems do not always disappear because somebody forgets the issue entirely.
Sometimes the information was communicated, but the incoming team understood something different from what the outgoing team intended.
The solution is not necessarily another factory-management application.
It starts with making every important unfinished issue visible, understandable and assigned to the right person.
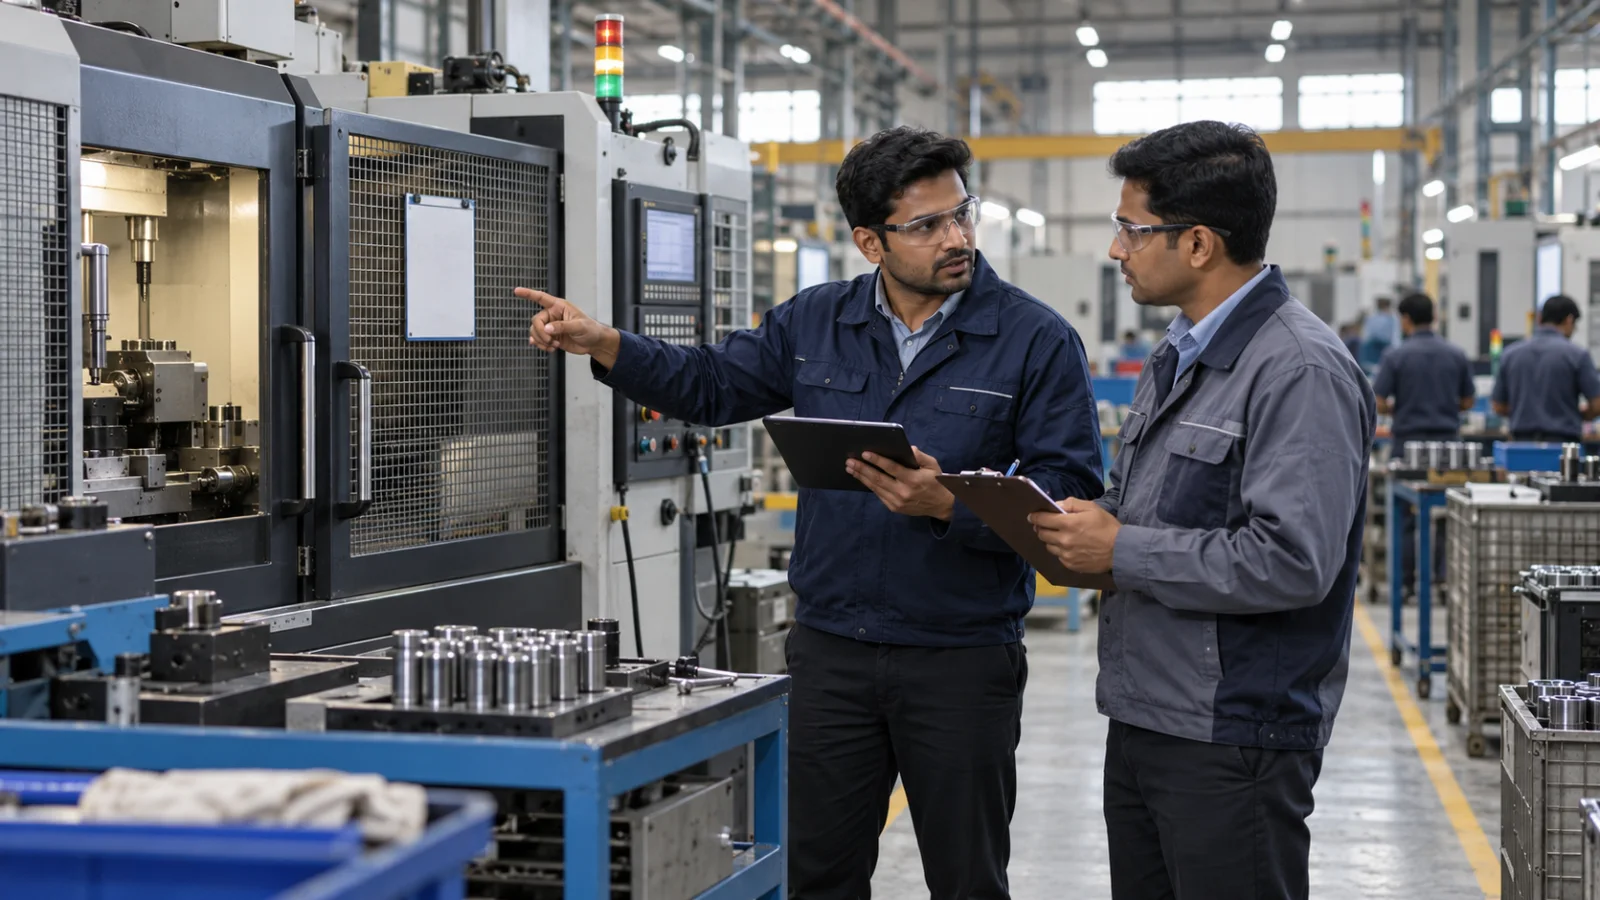
Cover image: AI-generated editorial illustration. The factory, employees and equipment shown are fictional and do not represent a GreyBath client or certify equipment safety.
A production report and a shift handover are not the same thing
Many factories already maintain daily production reports.
These reports may contain:
- Production targets.
- Actual output.
- Machine utilisation.
- Rejected quantities.
- Downtime.
- Operator attendance.
- Material consumption.
These are useful records.
But they mainly describe what happened during a period.
A shift handover has another purpose.
It must establish what the next team needs to know and what responsibilities continue after the current team leaves.
Consider two reports.
Report A: Production summary
Machine M-03.
Target: 500 components.
Produced: 320 components.
Machine stopped at 2:20 PM.
This tells management what happened.
Report B: Operational handover
Machine M-03 stopped following an abnormal-noise report.
Maintenance request MNT-081 remains open.
The machine has not been authorised to return to service.
Production order WO-482 remains incomplete.
The incoming supervisor must coordinate with the authorised maintenance team before any return-to-service decision.
This tells the incoming team what remains unresolved.
Both reports are useful.
But the second carries information necessary for continuing the work responsibly.
A factory needs to distinguish historical reporting from responsibility transfer.
Why verbal communication alone is unreliable
Imagine a production supervisor managing eight machines.
During the shift, several small issues occur.
One machine requires adjustment.
Another is waiting for material.
A third has an unresolved maintenance request.
One production order changes priority.
An operator reports an unusual vibration.
At the end of the shift, the supervisor must remember which information matters to the incoming team.
If the handover consists of a rushed conversation, details can easily become unclear.
The outgoing supervisor may believe the important information was communicated.
The incoming supervisor may believe the situation is under control.
Neither may realise that they understand the outstanding issue differently.
What established guidance recommends
The UK's Health and Safety Executive identifies three important elements of shift handover:
- Preparation by the outgoing personnel.
- Communication between outgoing and incoming personnel.
- Cross-checking by the incoming personnel as responsibility transfers.
It also recommends that handover be two-way and supported by both verbal and written information. HSE
These principles are relevant to ordinary manufacturing operations, although specific safety and compliance procedures depend on the factory and jurisdiction.
For an SME, the practical lesson is straightforward.
Do not depend on somebody remembering everything.
Do not depend on the incoming employee merely saying that the information was received.
Create a process in which the next team can understand and confirm the outstanding work.
The handover should focus on unfinished issues
A factory can produce hundreds of entries in a normal working day.
Not every routine activity needs to be discussed again at shift change.
The useful handover information is what the incoming team needs to operate responsibly and continue important work.
For example:
| Area | Information requiring handover |
|---|---|
| Production | Incomplete orders, changed priorities and work awaiting a decision |
| Maintenance | Open machine problems, work in progress and return-to-service authorisation status |
| Quality | Pending inspections, reported defects and unresolved quality decisions |
| Materials | Shortages or supply constraints affecting the next shift |
| Workforce | Approved staffing or skill-coverage issues affecting assigned work |
| Safety | Relevant hazards, restrictions and safety-critical work requiring formal continuity |
| Management decisions | Pending approvals or instructions affecting production |
The objective is not to create a long report for every shift.
It is to identify the information that must not disappear when the people change.
A useful handover record should be short enough to use consistently but complete enough to support the next action.
Distinguish reported, assigned and resolved issues
One reason factory reports become unreliable is that employees use vague statuses.
Consider a maintenance problem.
The operator reports an unusual sound.
The supervisor informs maintenance.
The technician visits the machine.
The outgoing supervisor writes:
Maintenance informed.
- What does that mean?
- Has the equipment been inspected?
- Was a fault identified?
- Has repair work started?
- Is the machine available for production?
- Is another assessment required?
- Who is responsible for the next decision?
A single status such as “Informed” does not answer these questions.
A more useful issue-status model
| Status | Meaning |
|---|---|
| Reported | An issue has been recorded |
| Assigned | An authorised person or team has responsibility |
| In progress | The responsible team is working on the issue |
| Awaiting decision | Further inspection, information or approval is required |
| Resolved | The defined issue has been addressed with supporting evidence |
| Closed | The required completion checks and authorised closure are recorded |
These are suggested workflow statuses, not standardised machine-safety states.
A machine being marked “Resolved” in a general issue tracker must never automatically mean it is safe or authorised to operate.
Equipment return-to-service decisions belong to the authorised personnel following the factory's applicable safety and maintenance procedures.
The handover system should display that decision.
It must not replace it.
A practical example: one unfinished production order and one machine issue
Consider a fictional company called Western Precision Components Pvt Ltd.
It manufactures industrial metal components for equipment manufacturers.
The factory operates two shifts.
This is a hypothetical example, not a GreyBath client project.
The first shift runs from 7:00 AM to 3:00 PM.
The second shift runs from 3:00 PM to 11:00 PM.
During the first shift, Machine M-03 develops an abnormal noise.
The supervisor stops the affected operation under the factory's established procedure and requests maintenance support.
Maintenance begins investigating.
The production order remains incomplete.
The production position
| Item | Quantity |
|---|---|
| Production order target | 500 components |
| Components physically produced | 320 |
| Components accepted by Quality | 300 |
| Components awaiting quality assessment | 20 |
| Components not yet produced | 180 |
These figures are hypothetical.
The 20 components awaiting assessment are included in the 320 physically produced units.
Therefore:
320 produced + 180 not yet produced = 500 planned components.
But only 300 have been accepted so far.
The remaining 200 components needed to reach 500 accepted units consist of 180 not yet produced and 20 awaiting assessment. Whether those 20 are eventually accepted is still unknown.
That distinction should remain visible.
The shift handover must not represent all 320 produced components as quality-approved.
The maintenance position
Machine M-03 has been stopped following the abnormal-noise report.
A maintenance request has been raised.
The technician has not yet completed the required assessment.
There is no authorised release for the machine to return to production.
The incoming supervisor must understand that the production order remains unfinished and that the machine's operating restriction remains in effect.
What the outgoing shift records
| Field | Handover information |
|---|---|
| Shift | Morning |
| Equipment | M-03 |
| Production order | WO-482 |
| Maintenance request | MNT-081 |
| Issue | Abnormal noise reported; operation stopped |
| Current equipment position | Not released for operation |
| Production completed | 320 components |
| Quality accepted | 300 components |
| Quality assessment pending | 20 components |
| Production not yet completed | 180 components |
| Maintenance owner | Authorised maintenance supervisor |
| Incoming production owner | Evening-shift supervisor |
| Next action | Obtain maintenance and production-authorisation update; maintain operating restriction until formally cleared |
| Handover status | Awaiting incoming-shift acknowledgement |
The record should reference the actual machine-maintenance and safety documents where applicable.
It should not attempt to replace formal equipment-isolation, inspection or release procedures.
What the incoming shift confirms
The incoming supervisor reviews the open issues and confirms that the handover has been understood.
They verify that Machine M-03 is still restricted from operation.
They establish which person is responsible for obtaining the maintenance update.
They also confirm the separate production and quality positions.
The incoming shift can plan other authorised work while the affected machine remains unavailable.
No unsafe restart or unsupported production commitment is assumed.
What management gains
Management now has a documented operational position.
It can see that the production order is incomplete.
It can identify the open maintenance request.
It can see who owns the next action.
And it can distinguish a handover that has been acknowledged from a machine that has been formally cleared.
The benefit is not that the issue has magically been solved.
The benefit is that the next shift knows the issue exists and who must resolve it.
Acknowledging a handover is not the same as completing the work
This distinction deserves attention.
Suppose the incoming supervisor clicks:
Handover accepted.
What should that mean?
It should mean that the incoming supervisor has reviewed and acknowledged the relevant handover information.
It should not mean:
- The maintenance problem is repaired.
- The quality issue is approved.
- The production order is completed.
- The machine is authorised to operate.
These are separate operational decisions.
A useful system therefore records two different things.
Handover acknowledgement: The incoming team has received and understood the outstanding information.
Issue resolution: The responsible person has completed the required work and recorded the relevant decision or evidence.
An unresolved issue can pass through several shift changes.
Its original reference should remain intact.
This helps prevent the same problem from being recorded repeatedly as unrelated new incidents.
Do not create a new maintenance complaint every shift
Imagine a machine developing the same fault during the morning shift.
The morning supervisor raises a maintenance request.
The evening supervisor raises another request because the machine is still unavailable.
The next morning, another employee creates a third request.
Management now sees three maintenance complaints.
But the factory may have only one unresolved underlying issue.
Repeated complaints can be useful evidence of recurrence, but duplicate independent records can distort reporting.
The business should define when an employee should:
- Update an existing open issue.
- Record a new occurrence linked to a previous issue.
- Create a genuinely new issue.
For example, an unresolved maintenance request should normally remain linked to the original reported problem.
If the equipment was repaired, formally released and subsequently developed another problem, that may justify a new incident linked to the earlier history.
The correct classification depends on the circumstances.
Why the original reference matters
A stable issue reference helps management understand:
- When the problem was first reported.
- How many shifts have handled it.
- Which teams were involved.
- What actions were completed.
- What remains pending.
- When the final outcome was authorised.
Without that history, recurring problems can look like unrelated daily events.
Give the next action to a named owner
Many handover reports use phrases such as:
- Maintenance will check.
- Quality to confirm.
- Material pending.
- Production to follow up.
These statements identify a department.
They do not necessarily establish responsibility.
A useful record identifies a person or defined role responsible for the next action.
For example:
| Issue | Current owner | Next action |
|---|---|---|
| Machine M-03 unavailable | Maintenance supervisor | Complete assessment and record authorised equipment status |
| Inspection pending | Quality supervisor | Record inspection outcome for the identified components |
| Production order incomplete | Incoming production supervisor | Review the authorised production plan |
| Material requirement unresolved | Stores coordinator | Confirm material availability and communicate the result |
A responsible employee does not need to perform every task personally.
They do need to ensure that the required action is followed through.
When the designated employee is unavailable, the business should have an authorised escalation route.
This is especially important for small factories where one technician or supervisor may handle several responsibilities.
How a small factory can organise its shift handover
A useful process has three connected parts.
Before the outgoing shift finishes
The supervisor reviews the current production position and identifies work that cannot be considered complete.
They confirm which maintenance, quality, material and safety-related issues remain open.
The relevant issue records should be updated with the known facts.
Where an issue requires formal authorisation, its actual approval status must be recorded or referenced correctly.
Do not mark a problem resolved merely because the responsible employee has been informed.
During the handover
The outgoing and incoming supervisors discuss the important open items.
The conversation should focus on what changed, what remains unresolved and who owns the next action.
Higher-risk matters require the appropriate level of direct communication and verification.
A shared register supports this discussion.
It should not replace required face-to-face or formal safety handovers.
The HSE's guidance emphasises preparation, two-way communication and cross-checking, rather than relying on one-way written messages. HSE
After the incoming shift takes responsibility
The incoming supervisor checks the relevant information and acknowledges the transfer.
They verify important restrictions and pending decisions through the appropriate sources.
Open work remains visible until the authorised person records the required outcome.
Where an issue crosses another shift boundary, its responsibility is transferred again without losing the original history.
This creates continuity.
The shift ends.
The issue record does not automatically end.
A practical shift-handover template
A small manufacturing company can begin with a paper logbook or controlled spreadsheet.
The following structure is intended as an operational working template.
| Field | What to record |
|---|---|
| Date and shift | Shift to which the handover relates |
| Machine or work area | Equipment, production line or department |
| Production order | Relevant work-order reference |
| Issue ID | Stable reference for the outstanding problem |
| Issue description | Specific observed problem |
| Current operational position | What is confirmed at handover |
| Relevant restriction | Any applicable hold or restriction, referencing the authoritative procedure |
| Responsible person | Who owns the next action |
| Next action | What must happen next |
| Required review time | When the issue needs to be reviewed |
| Outgoing supervisor | Person communicating the handover |
| Incoming supervisor | Person receiving responsibility |
| Acknowledgement | Confirmation that the information was reviewed |
| Resolution reference | Evidence of final authorised closure when completed |
Not every issue requires every field.
For routine non-critical matters, a shorter record may be sufficient.
For safety-critical or regulated activities, a generic template may be insufficient and must not replace mandatory workplace procedures.
The purpose is to make the record match the information required for the next shift to work responsibly.
Why a WhatsApp group may not be enough
Many smaller factories use WhatsApp groups to coordinate production.
This can be convenient.
- Employees can share photographs.
- Supervisors can report delays.
- Maintenance teams can receive messages quickly.
However, an informal group is not automatically a dependable issue-management system.
Imagine messages such as:
Machine 3 issue.
Technician checking.
Any update?
Will confirm.
Night shift check once.
Which message represents the latest verified position?
Who owns the issue?
Was the restriction lifted?
When was the problem formally closed?
A chat history may contain the information somewhere, but employees must reconstruct the situation from individual messages.
Use messaging for communication, not as the only authoritative record
A practical arrangement is to maintain the issue in one approved register.
The WhatsApp group may be used to alert the responsible person to review that record, where permitted by company policy.
Important decisions should remain documented in the appropriate operational or safety system.
Do not assume that somebody reading a WhatsApp message means they have accepted responsibility for an equipment or safety handover.
The distinction matters.
Communication is one activity.
Acknowledgement and authorisation are different activities.
When the outgoing supervisor is absent
Not every handover happens under ideal circumstances.
An employee may become unavailable.
A shift may be extended unexpectedly.
An urgent issue may require immediate escalation.
The business needs a procedure for these exceptions.
For example, if the outgoing supervisor cannot conduct the planned handover, an authorised replacement should review the available records and coordinate the necessary transfer.
The incoming team should not assume that missing information means there are no open issues.
If equipment status or safety information cannot be established, the matter should be escalated through the factory's applicable procedure before the affected operation continues.
For safety-critical work, the UK HSE and the US Occupational Safety and Health Administration both emphasise continuity of protective information and procedures during personnel changes.
OSHA's lockout/tagout requirements are US regulations, not Indian legal requirements. They are cited here as an additional example of why a general shift log cannot replace a formal hazardous-energy-control procedure. OSHA
For an Indian factory, applicable Indian law, equipment-specific requirements and the organisation's authorised safety procedures must govern the actual work.
Start with one production area before changing the whole factory
A company with 20 machines does not need to launch a factory-wide software project immediately.
Select one production area where unfinished issues frequently cross shifts.
- Use the existing register or introduce a simple controlled log.
- Agree on the information to be recorded.
- Identify who prepares the handover.
- Identify who receives it.
- Define how outstanding issues are carried forward.
- Explain which approvals cannot be given through the handover record.
Then observe how employees use the process.
What management should learn from the pilot
- Are the handover records understandable?
- Do incoming employees know the next action?
- Are maintenance issues linked to the original request?
- Are employees creating duplicate complaints?
- Is the responsible person clearly identified?
- Are safety-related restrictions preserved through the shift change?
- Are important issues remaining open without any review?
These questions reveal whether the process is useful.
Do not judge success merely by the number of forms completed.
A handover form has value only when it improves the transfer of relevant information and responsibility.
Check whether your existing software already supports the workflow
Before buying a new application, examine the software already in use.
Your factory may have:
- An ERP.
- A production-planning system.
- A maintenance module.
- A quality-management application.
- An internal task register.
Some of the required capabilities may already exist.
For example, Odoo 19 documents maintenance requests that can be associated with equipment, work centres, manufacturing orders and work orders.
Its maintenance process also supports assigning responsible teams and managing request stages. Odoo
That does not mean Odoo automatically provides the entire shift-handover process described here.
It means that the maintenance part of the problem may already have a structured home.
Avoid duplicating the same information
Suppose the ERP already contains maintenance request MNT-081.
The shift log should reference that request.
Employees should not need to manually maintain a second independent description of the same maintenance work.
Similarly, if the production system already records completed quantities, the handover view should use the verified information from that system where practical.
The objective is to connect existing records around the next action.
Not to create another system that makes employees enter the same information twice.
When a spreadsheet is sufficient
A controlled spreadsheet may work for a small workshop operating two shifts.
It can record open issues, owners, review dates and handover acknowledgement.
For non-critical administrative issues, this may provide the required visibility.
However, a spreadsheet becomes more difficult when several supervisors update it simultaneously, multiple production lines use different registers or the process requires detailed access control.
There is also a difference between a spreadsheet that records routine follow-up and one being relied upon for safety-critical operating decisions.
For the latter, use the authorised safety and maintenance procedures and systems.
Do not depend on an editable spreadsheet as the sole control preventing unsafe operation.
When a connected shift-management workflow becomes useful
A connected application becomes more relevant when the information exists across several systems and departments.
For example:
- ERP: Production orders and quantities.
- Maintenance system: Machine problems and repair requests.
- Quality system: Inspection results and pending decisions.
- Supervisors: Shift observations and outstanding work.
- Management: Requires one view of unresolved issues and responsibilities.
A connected workflow could bring together relevant references, statuses and next actions.
However, the project must establish which system owns each decision.
The ERP may own production quantities.
The maintenance system may own repair records.
The safety process may govern machine restrictions and return-to-service authorisation.
The handover workflow may own acknowledgement and transfer of operational responsibility.
A dashboard should not become the authority for decisions that belong to a separate controlled process.
Questions to answer before development
- Can the existing systems provide the required records through supported APIs or authorised exports?
- Are machine IDs and work-order references consistent?
- Which employees can record and edit issues?
- Who can acknowledge handovers?
- Who can close each category of issue?
- What happens if a system is unavailable?
- How are corrections recorded without erasing the original history?
- What does the incoming shift see when information has not been updated?
These requirements should be defined before selecting the technology.
Keep the digital process usable on the factory floor
A factory-floor application is not useful merely because it has a modern dashboard.
Employees may work while wearing protective equipment.
They may use shared terminals.
Some areas may have weak mobile connectivity.
Supervisors may have limited time for data entry.
An effective interface should support the actual work environment.
For example, an employee should be able to identify the correct machine and issue without navigating through unnecessary screens.
Open issues should remain visible when a new shift begins.
Critical restrictions should not disappear because an ordinary notification has been dismissed.
If offline recording is supported, the system should clearly distinguish information saved locally from information successfully synchronised.
When a connection fails, staff must have an approved alternative process for transferring essential information.
Technology can improve visibility.
It cannot guarantee that employees will use the correct procedure.
Measure the quality of handovers, not the number of entries
Once the process has been introduced, management can review whether responsibilities are being transferred more reliably.
Use a small number of meaningful measures.
Open issues without incoming acknowledgement
Track issues carried into the next shift without the required acknowledgement.
For example, if 12 issues required handover and 10 were acknowledged under the defined procedure, the acknowledgement rate is:
10 ÷ 12 × 100 = 83.3%
This is a hypothetical calculation.
It measures process completion.
It does not prove that the acknowledged information was accurate or that the issues were resolved.
Safety-critical exceptions should be reviewed individually rather than treated as acceptable because the overall percentage appears high.
Open issues without a responsible owner
Identify unresolved items with no person or defined role accountable for the next action.
This helps management distinguish a genuine technical delay from a responsibility gap.
Issues carried across multiple shifts
Measure how long important issues remain open and how many shift changes they pass through.
A long-running issue is not automatically evidence of employee failure.
Some work legitimately requires parts, specialist inspection or scheduled repair.
The measure should help management understand why the issue remains unresolved.
Repeated reports of the same problem
Review recurring equipment complaints.
Determine whether they represent unresolved issues, repeated failures or duplicate records.
This can help management investigate underlying problems without artificially inflating incident counts.
Production interruptions linked to communication failures
Where evidence supports the classification, record interruptions caused or extended by incomplete handover information.
Do not attribute every machine stoppage to a handover failure.
A mechanical fault and a communication failure may be separate issues.
Handover exceptions requiring escalation
Track significant cases where the normal transfer process could not be completed.
Review whether the appropriate authorised escalation occurred.
The purpose is to improve the process, not merely to reduce the reported number of exceptions.
When a digital handover system will not solve the problem
A shift-management application cannot repair a defective machine.
It cannot replace a trained maintenance technician.
It cannot establish that an unsafe operation may resume.
It cannot authorise a quality release.
And it cannot make an employee competent to perform work for which they have not been trained.
The system can record and communicate decisions.
Those decisions must still come from the appropriate people and procedures.
Some factories also require specialised controls involving hazardous equipment, chemicals, pressure systems, electrical work or regulated manufacturing processes.
For those environments, the handover process must be designed around the applicable safety, technical and regulatory requirements.
A general digital form is not a safety certification.
The same applies to factories with only one shift.
Such businesses may not need a shift-change process, but they may still benefit from controlled handovers between production, maintenance and quality teams.
The principle is continuity of responsibility.
It is not limited to employees changing duty hours.
The important management decision
When a factory changes shifts, employees should not have to reconstruct unfinished work from memory.
The outgoing team should know what information must be transferred.
The incoming team should know what remains unresolved.
The responsible person should be identifiable.
Important restrictions should remain in force until the appropriate authorised decision changes them.
And the original issue should retain its history across shifts.
Start with one production area.
Use existing records.
Create a clear handover process.
Review whether incoming employees understand their responsibilities.
Only consider additional software when the manual process becomes difficult to maintain.
A factory shift should transfer responsibility for unfinished work—not make the unfinished work disappear.
Where GreyBath can contribute
GreyBath develops custom web applications, ERP workflows, dashboards, mobile applications and system integrations.
For small and medium-sized manufacturers, a potential GreyBath implementation could connect production records, maintenance requests and shift-level follow-up activities into a shared operational workspace.
Depending on the factory's existing systems, this could include digital handover records, issue assignment, incoming-shift acknowledgements, unresolved-task alerts, role-based permissions and management dashboards.
A mobile-friendly interface could support supervisors recording and reviewing information on the shop floor. Where supported APIs or authorised exports exist, GreyBath could assess integration with the company's existing ERP or maintenance application rather than replacing those systems.
The implementation would require clear process ownership, permission rules, reliable source data and appropriate treatment of safety-related information.
GreyBath would not replace the factory's authorised maintenance, quality or safety decision-makers.
For a smaller operation, a structured existing logbook or configured software module may be sufficient.
GreyBath's relevant contribution begins when the factory needs a dependable way to connect existing operational information with responsibilities that continue across shifts.
Keep reading
More practical thinking from GreyBath across design, engineering and growth.
All articles